


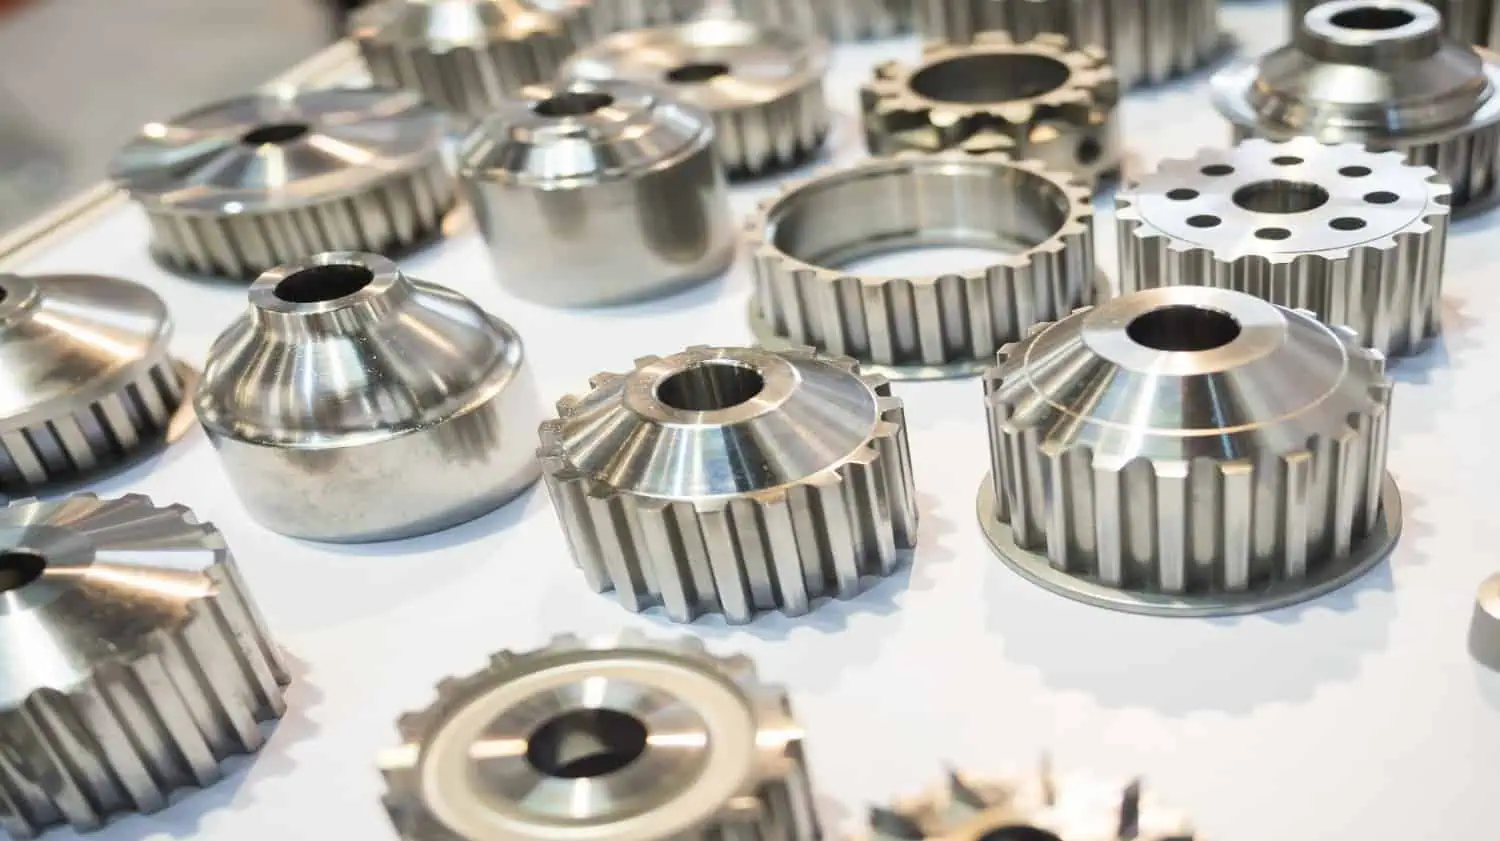
The centrifugal casting vs sand casting strength comparison often comes down to something you can’t see on a spec sheet: where the impurities end up. I’ve watched procurement teams approve a sand-cast sleeve based on a $2,000 pattern tooling cost, only to discover 18 months later that porosity in the cross-section caused a field failure at 200 hours. The $15,000 in lost production and warranty calls wiped out the tooling savings five times over. That’s the reality behind the 10-20% tensile strength gap that metallurgists cite.
The real difference isn’t just grain size — it’s process physics. Centrifugal casting spins the mold at 300-1500 RPM, forcing inclusions to the inner bore where machining removes them. Sand casting leaves those same impurities distributed through the wall section, waiting to crack under load. For a 50 kg pump sleeve, the breakeven volume where centrifugal casting becomes cheaper than sand casting is roughly 500 units, once you factor in the 1-5% scrap rate for weld-repair and the 3-5 mm of extra machining waste per face. Most buyers never run that total landed cost calculation.
Why Centrifugal Casting Produces a Denser Grain Structure
Centrifugal casting produces ASTM 5-7 grain size, two grades finer than sand casting — directly translating to a 30% increase in fatigue.
The difference starts with physics. In centrifugal casting, the mold spins at 300-1500 RPM. Molten metal is thrown outward against the die wall by centrifugal force — the same force that pins you to the wall on a carnival ride. That pressure forces the metal to solidify rapidly from the outer surface inward.
How the Spin Creates a Finer Microstructure
Rapid solidification at the mold wall drives nucleation — more crystals form, but they don’t have time to grow large. The result is a grain size of ASTM 5-7. Compare that to sand casting, where cooling is slower and uncontrolled: grains reach ASTM 3-5, meaning fewer, larger crystals with weaker grain boundaries between them.
There’s a second mechanism at work. As the metal spins, lighter impurities and gas bubbles migrate toward the inner bore. They concentrate there because centrifugal force pushes denser material outward. That inner layer gets machined away in post-processing. What remains is a defect-free outer zone with no porosity inclusions waiting to initiate cracks.
The Grain Size vs. Fatigue Life Trade-off
Finer grain structure means more grain boundaries per unit volume. Each boundary acts as a barrier to dislocation movement under cyclic stress — which is exactly how fatigue cracks propagate. More barriers = longer fatigue life. Internal production data from Kbear Metal shows a measurable 30% increase in fatigue life for rings and sleeves made via centrifugal casting compared to sand casting with identical alloy composition.
That number matters when you’re sourcing pump sleeves, bearing journals, or any rotating component where failure means unplanned downtime and replacement labor. A sand-cast sleeve that fails at 200 hours due to internal shrinkage porosity costs $15,000 in lost production alone — not counting the part itself or the service call.
- Grain Size (ASTM): Centrifugal: 5-7 | Sand: 3-5.
- Porosity Rate: Centrifugal: <0.5% | Sand: 1-5%.
- Fatigue Life Gain: Centrifugal delivers up to +30% vs sand (rings/sleeves).
- Impurity Location: Centrifugal: trapped at bore (machined away) | Sand: distributed through cross-section.
Where Sand Casting Still Wins—Size, Shape, and Setup Costs
Sand casting wins on size and setup cost, but the total cost story flips above 500 units.
The Cost Advantage of Sand Patterns
A sand casting pattern costs between $500 and $10,000. A permanent die for centrifugal casting runs $10,000 to $100,000. That spread is the main reason procurement teams default to sand for low-volume runs. Sand casting also handles parts up to 10,000 kg — centrifugal casting tops out around 10 tons for cylindrical sections. For large, complex enclosures or brackets with internal cores, sand casting is the only option.
- Pattern tooling cost: Sand: $500–$10,000 | Centrifugal: $10,000–$100,000.
- Maximum part weight: Sand: up to 10,000 kg | Centrifugal: ~10 tons (limited by mold spin dynamics).
- Geometric complexity: Sand: handles internal cores, non-cylindrical shapes | Centrifugal: rotationally symmetric only.
- Machining allowance: Sand: 3–5 mm per face | Centrifugal: 1–2 mm per face (outer zone already defect-free).
- Porosity rate: Sand: 1–5% require weld repair | Centrifugal: <0.5%.
- Breakeven volume (50 kg sleeve): Centrifugal becomes cheaper than sand at ~500 units including rework and scrap.
The Hidden Cost of Machining and Rework
The cheap pattern starts looking expensive when you add machining. Sand castings require 3–5 mm of stock removal per face to reach the final dimension. That wastes material and machine time. Worse, 1–5% of sand castings have porosity that needs weld repair. Each porosity reject triggers rework, extra inspection, and potential field failures. A sand-cast pump sleeve failed after 200 hours in a concrete batching plant, costing $15,000 in lost production.
Kbear Metal’s foundry engineers review every part drawing before production, analyzing riser placement and gating to minimize porosity in sand casting. But for cylindrical parts under high stress or pressure, the only way to guarantee <0.5% porosity is to switch to centrifugal casting. The breakeven point for a typical 50 kg sleeve is around 500 units — after that, the total landed cost of centrifugal casting (including machining savings and scrap reduction) beats sand casting.
| Feature | Sand Casting | Centrifugal Casting | Why It Matters |
|---|---|---|---|
| Maximum Part Size | Up to 10,000 kg (10 tons) | ~10 tons; 3m diameter x 15m length | Sand casting handles large, complex housings; centrifugal is limited to cylindrical shapes. |
| Shape Complexity | High (complex internal cores, flanges, bosses) | Low (rotationally symmetric only) | For non-cylindrical parts with intricate geometry, sand casting is the only option. |
| Pattern / Die Cost | $500 – $10,000 (pattern tooling) | $10,000 – $100,000 (permanent die) | Sand casting is far cheaper for low-volume or one-off parts. |
| Setup & Lead Time | Fast (patterns can be made in days) | Slower (die fabrication takes weeks) | Sand casting wins for urgent prototypes or small batches. |
| Machining Allowance | 3–5 mm per face (more waste) | 1–3 mm per face (less waste) | Sand casting’s ‘cheap’ mold hides higher machining costs and material loss. |
Field Failure Example: Sand-Cast Sleeve Failed After 200 Hours
A sand-cast pump sleeve failed at 200 hours, costing $15,000 in lost production.
A concrete batching plant in Texas installed a sand-cast pump sleeve from a low-cost supplier. At 200 hours of operation, the sleeve cracked under pressure. The internal shrinkage porosity — invisible on the surface during incoming inspection — had created a network of voids that propagated into a fatigue failure. The plant lost two shifts of production while the line sat idle. Total cost: $15,000 in downtime alone, plus replacement part and labor.
Why Porosity Kills Cylindrical Parts Under Load
Sand casting cools slowly under gravity. Gas bubbles and shrinkage voids form inside the cross-section, concentrated near the center of thick walls. In a cylindrical sleeve under pressure or rotation, those voids act as stress risers. The crack initiates at the void boundary and propagates through the wall. Centrifugal casting solves this by spinning the mold at 300–1500 RPM. The centrifugal force pushes molten metal outward, trapping gas and inclusions at the inner bore where machining removes them.
The result is a defect-free outer zone with grain sizes of ASTM 5–7 — two grades finer than typical sand castings. That translates to 10–20% higher tensile strength and up to 30% longer fatigue life for rings and sleeves.
How to Avoid This Failure on Your Next Order
First, specify centrifugal casting for any cylindrical part exposed to high stress or pressure — pump sleeves, bearing journals, ring flanges, hydraulic cylinders. Sand casting cannot guarantee <0.5% porosity in axisymmetric sections; centrifugal casting can.
Second, insist on porosity testing before shipment. X-ray or ultrasonic inspection will reveal internal voids that visual checks miss. Request a grain structure report alongside the material certificate so you can verify ASTM grain size meets your design requirements.
Conclusion
The choice between centrifugal and sand casting comes down to one question: where do you want the impurities to end up? Centrifugal casting forces them to the bore, where machining removes them. Sand casting leaves them scattered through the cross-section, waiting to become a crack initiation site under load. That single difference drives the 10-20% tensile gap and the 30% fatigue life improvement.
- Centrifugal casting delivers <0.5% porosity vs. 1-5% for sand.
- Grain size runs ASTM 5-7 for centrifugal, two grades finer than sand.
- Breakeven volume for a 50 kg sleeve is roughly 500 units.
If you skip the process analysis and default to sand casting because the pattern costs less, you are betting that porosity won’t show up in your part. That bet fails at 1-5% of the time — and each failure triggers welding, rework, and a field warranty call that wipes out the pattern savings. The cost of inaction is a sand-cast sleeve failing at 200 hours, costing $15,000 in lost production. Upload your part drawing and load spec to Kbear Metal. The engineering team will review the grain structure, porosity risk, and casting economics, then recommend the process that keeps your part from failing in the field. Contact [email protected].
Frequently Asked Questions
Is centrifugal casting stronger than sand casting?
Yes, centrifugal casting is typically 10-20% stronger in tensile strength due to a finer grain structure and lower porosity. This makes it the preferred choice for pressure-tight or rotating parts like. Choose centrifugal for high-stress cylindrical parts; sand casting for complex shapes.
What is the maximum size for centrifugal casting?
Centrifugal casting is generally limited to cylindrical parts up to about 6 meters in length and 3 meters in diameter. For larger or more complex geometries, sand casting remains the only viable. Confirm size limits with your foundry before finalizing the design.
Why do sand castings have porosity?
Porosity in sand castings occurs because gas gets trapped as the molten metal cools unevenly in the sand mold. This typically results in 1-5% of pieces needing weld repair or rework, adding. Expect porosity in sand castings and budget for potential rework.
Which casting method is cheaper for low volume production?
Sand casting is cheaper for low volume production because pattern tooling costs only $500-$10,000 versus $10,000-$100,000 for centrifugal dies. However, the cost advantage flips above 500 units when. Use sand casting for prototypes or small batches; switch to centrifugal for higher volumes.
Can centrifugal casting produce custom, non-cylindrical parts?
No, centrifugal casting is inherently limited to cylindrical or symmetrical shapes due to the spinning mold process. For custom, non-cylindrical parts, sand casting or investment casting are the practical alternatives. Stick with sand casting for complex geometries and custom shapes.



