


Premier Ethylene Cracking Furnace Tubes — HK40, HP-Nb & Modified Alloy Centrifugal Cast
Kbear Metal manufactures centrifugally cast cracking coil tubes for ethylene, propylene, and pyrolysis furnaces. HK40, HP-Nb, and modified-alloy grades cast to ASTM A608 — service temperatures 1,000-1,150°C, creep-rupture data per ECSC-NESC database, and ID surface engineered for coking resistance.
// Cracking Tube Spec
Metrics that matter for ethylene plant tube buyers
Hard numbers that define what we can supply for cracking coil and pyrolysis tube projects.
Max Coil Temp
HP-Nb alloy ceiling for ethylene cracking coil tubes in pyrolysis service.
Creep Design Life
Calculated creep-rupture life at design coil-wall temperature. API 530 verified.
OD Tolerance (mm)
As-cast OD held within ±0.4 mm after machining. Critical for coil assembly.
Max Tube Length
Single-piece centrifugal casting up to 12 m straight section.
UT Coverage
Ultrasonic testing on every cracking tube. No statistical sampling.
Hydrostatic Test
Pressure test at 1.5x design pressure per ASME B31.3 on every tube.
Mill Cert
EN 10204 3.1 chemistry and mechanical traced to heat number per coil.
Lead Time (days)
Standard HK40 / HP-Nb cracking tubes from confirmed PO to packed crate.
Six cracking tube configurations for pyrolysis service
Straight coils, return bends, U-bends, and outlet headers for ethylene, propylene, and naphtha cracking furnaces.
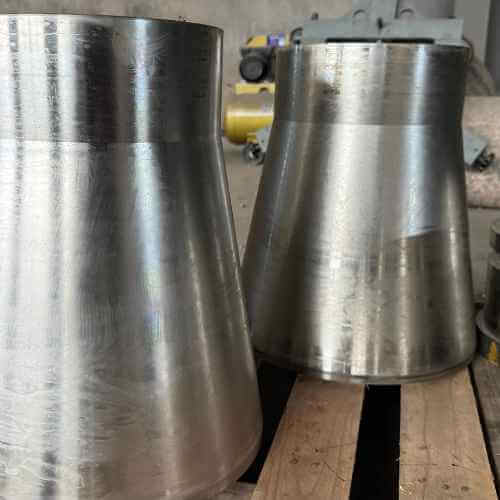
HK40 Cracking Coils
25Cr-20Ni alloy for ethylene cracking coil straight sections. Service to 1,100°C coil-wall temperature.
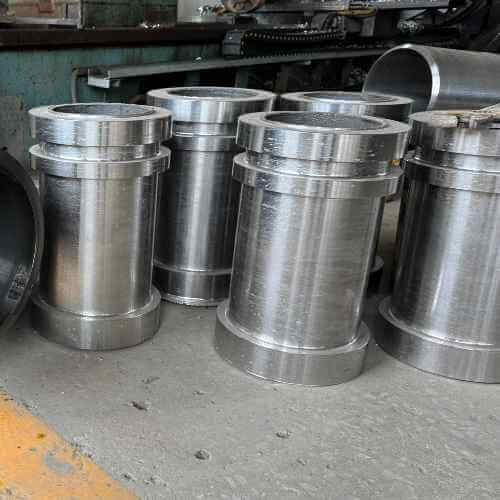
HP-Nb Pyrolysis Tubes
35Cr-45Ni-Nb modified alloy for severe pyrolysis service. Creep performance superior to standard HK40.
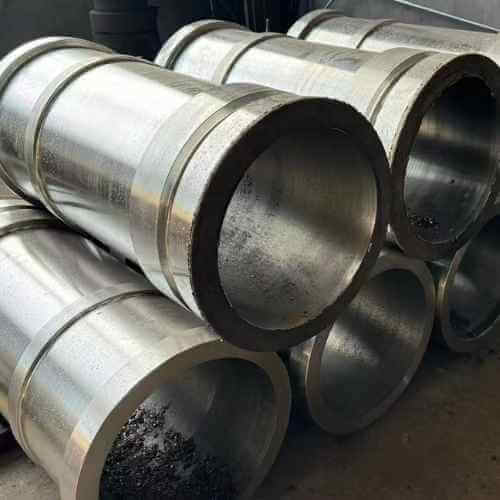
Return Bends & U-Bends
Coil return bends in matching HK40 / HP-Nb alloy. Cast as single piece — no welded miter joints.
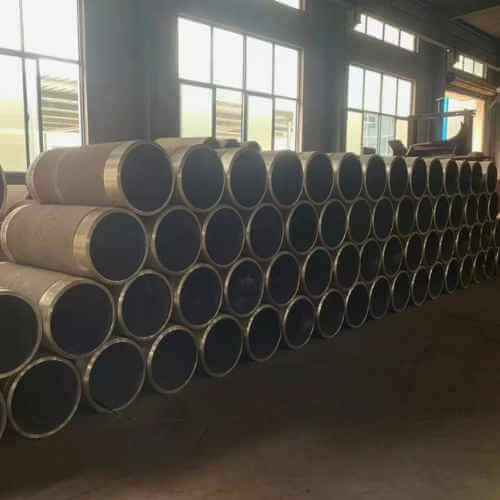
Coil Outlet Headers
Outlet collector headers for cracking coil assemblies. HP-Nb or Alloy 800H matching coil chemistry.
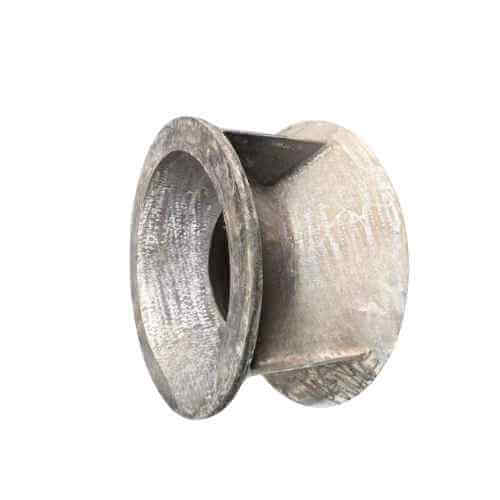
Propylene Cracking Tubes
HK40 and HP-Nb tubes for propane dehydrogenation (PDH) and propylene plant cracking service.
Anti-Coking ID Tubes
Cracking tubes with aluminized or silicon-doped inner surface for reduced coke deposition between decoking cycles.
From melt to packed coil — eight controlled stages
API 530 and ASME B31.3 documentation chain maintained at every stage.
Chemistry Design
Cr / Ni / Nb / C target ranges defined per ASTM A608 grade. Ladle sample verifies pre-pour.
Mold Prep
Sand-coated metal mold preheated to 200-400°C. Inner coating prevents alloy-mold reaction.
Induction Melt
Medium-frequency induction at 1,560-1,580°C. Argon purge removes dissolved hydrogen.
Centrifugal Pour
Mold at 700-1,300 RPM (matched to OD). Controlled pour rate via tundish.
Cooling & Demold
Controlled cooling prevents thermal cracking. ID rough-machined to remove inclusions.
Solution Anneal
Heat-treat at 1,150°C, hold per wall thickness, rapid cool. Documented thermal profile.
NDT & Pressure
100% UT and dye-penetrant. Hydrostatic test 1.5x design pressure per ASME B31.3.
Machine, Mark, Pack
OD/ID finish-machined, heat number stamped, end-protected, crated for export.
HK40, HP-Nb, and modified-alloy cracking grades
Material verified by spectrometer on every melt. PMI re-verification on shipped tubes available.
25Cr-20Ni
Standard cracking alloy. Service to 1,100°C.
25Cr-20Ni-Nb
Niobium-modified for improved creep.
25Cr-35Ni-Nb
Severe pyrolysis. Service to 1,150°C.
HP-Mod High-Ni
Anti-coking, lower carburization.
15Cr-35Ni
Higher Ni for carburization service.
19Cr-39Ni
Severe carburizing/sulfidizing.
Alloy 800H
Outlet headers and pigtails.
Buyer-spec alloys
Project chemistry per drawing.
Cracking tube dimensional and mechanical capability
Standard tube envelope. Custom dimensions and chemistry quoted on a project basis.
| Parameter | HK40 | HP-Nb | 35Cr-45Ni |
|---|---|---|---|
| Composition (Cr/Ni) | 25 / 20 | 25 / 35 / Nb | 35 / 45 |
| Max Coil Wall Temp (°C) | 1,050 | 1,150 | 1,150 |
| Tensile Strength (MPa) | 450 | 470 | 460 |
| Yield Strength (MPa) | 240 | 280 | 260 |
| Creep Rupture (10⁵ h, 1,000°C) | 8 MPa | 14 MPa | 16 MPa |
| Carburization Resistance | Standard | High | Very High |
| OD Range | 50-200 mm | 50-250 mm | 50-200 mm |
| Wall Thickness | 6-20 mm | 6-20 mm | 6-18 mm |
| Max Length (single piece) | 10 m | 12 m | 10 m |
Documentation chain that passes ethylene plant procurement audits
Cracking tube failures shut down ethylene production at $250,000+ per day lost margin. Procurement teams audit suppliers for full traceability — chemistry, heat treatment, NDT, pressure test. Our QC builds the package alongside production.
100% UT Inspection
Ultrasonic testing on every coil tube — not statistical sampling. Volume coverage 100%.
Hydrostatic Pressure Test
1.5x design pressure per ASME B31.3. Test certificate issued per tube with serial number.
Carburization Test Data
Carburization resistance test data per ASTM B619 protocol available on test heats.
Creep-Rupture Database
Long-term creep-rupture data per ECSC-NESC database. Useful for run-length modeling.
Heat Number Traceability
Every tube stamped with heat number traceable through ladle sample to raw material.
Where cracking tubes ship from our factory
Eight pyrolysis service applications where centrifugally cast cracking tubes are the industry standard.
Ethylene Plants
Ethylene cracking furnace coil tubes for steam cracker pyrolysis service.
Propylene PDH
Propane dehydrogenation reactor tubes for propylene plant production.
Naphtha Cracking
Naphtha-fed cracking furnace coils for olefin chemical complex feedstock.
Pyrolysis Furnaces
General pyrolysis furnace tubes for petrochemical feedstock conversion.
Ethane Cracking
Light-feed (ethane) cracking furnace coils for gas-cracker olefin plants.
BTX Aromatics
Reformer-section tubes for benzene-toluene-xylene aromatic plants.
Coker Furnaces
Delayed coker heater tubes — lower-temp variant with carburization resistance.
Specialty Petrochem
Specialty chemical pyrolysis — methanol-to-olefins, butadiene units.
See how a cracking coil tube gets made
Three short videos covering melt chemistry, centrifugal casting, and quality verification.

HK40 Chemistry Verify & Pour
Ladle spectrometer verifies 25Cr-20Ni composition before pour. Mold spins at 1,100 RPM.
Solution Anneal + UT Inspection
Tubes annealed at 1,150°C, then 100% ultrasonic testing on every tube before machining.
Hydrostatic Test + Export Pack
1.5x design pressure hydrostatic test per ASME B31.3, then end-protected and crated for sea freight.
Buyer questions, answered directly
Common questions from ethylene plant procurement engineers, EPC project buyers, and pyrolysis furnace maintenance teams.