


Leading Source for Petrochemical Centrifugal CastingsHP40 Reformers · HK40 Cracking Tubes · Refinery Furnace Components
Kbear Metal supplies centrifugally cast tubes and components to refineries, hydrogen plants, ethylene crackers, ammonia plants, and methanol producers across 40+ markets. HP40, HK40, HP-Nb, and Inconel grades cast to ASTM A608 with PED 2014/68/EU certification path. Full creep-rupture data per API 530 / ECSC-NESC.
"Tube failures shut down plants at $250K/day. Documentation is the difference between approved and rejected supplier."
EPC procurement teams audit every tube supplier. Our QC builds the documentation package alongside production — chemistry, NDT, pressure test, heat number.
Standards that pass refinery procurement audits
Petrochemical tube buyers audit suppliers against ASME, API, ASTM, and EN compliance. Our quality management system has been audited annually since 2010. Standard documentation supports all major refinery and EPC customer-specific requirements.
Heat-Resistant Castings
HP40/HK40/HP-Nb grade path. Mill cert per heat with chemistry traceability.
Tube Wall Design
API 530 design calculations included with quote for fired-heater tube applications.
EU Pressure Equipment
PED 2014/68/EU compliance for EU export. Notified body involvement supported.
Pressure Test Standard
Hydrostatic test at 1.5x design pressure per ASME B31.3 on every pressure tube.
3.1 / 3.2 Mill Cert
3.1 standard; 3.2 with third-party inspector sign-off available on request.
MR0175 Sour Service
NACE certification path for H2S-containing service applications in oil & gas.
Six petrochemical casting categories produced under one roof
From hydrogen reformers to ethylene crackers — every tube and component for refinery and petrochemical service.
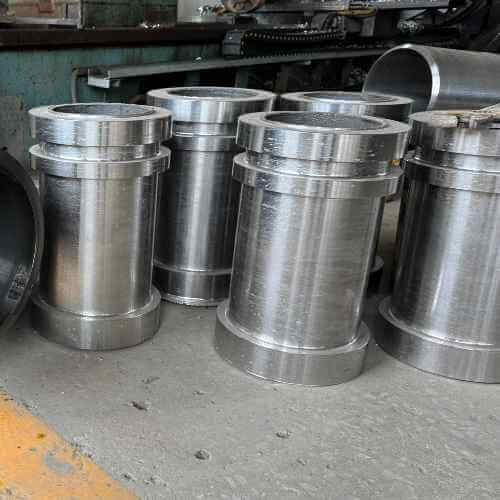
Reformer Tubes
HP40/HP-Nb tubes for hydrogen reformers, methanol synthesis, ammonia catalyst chambers.
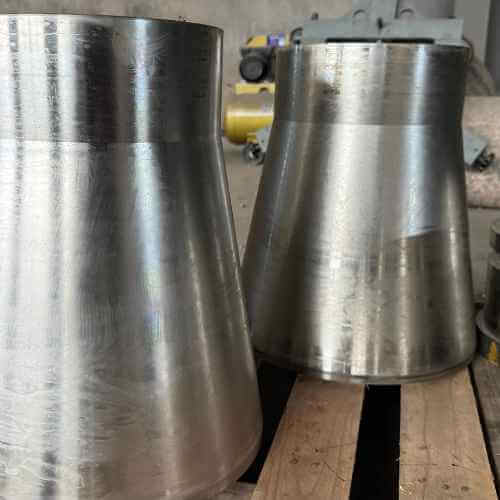
Ethylene Cracking Tubes
HK40/HP-Nb cracking coils for ethylene, propylene, and pyrolysis furnaces.
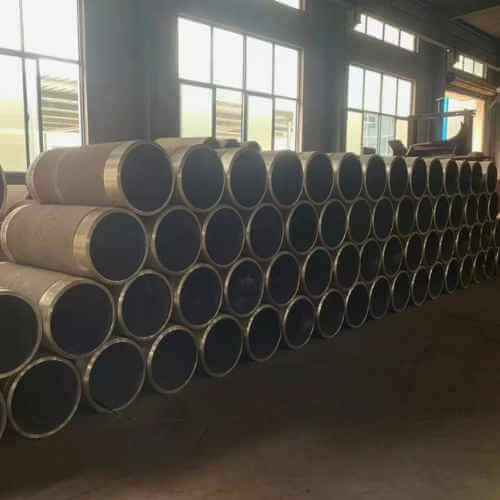
HP40 / HP-Nb Alloy
25Cr-35Ni heat-resistant castings for severe service reformer and high-temp applications.
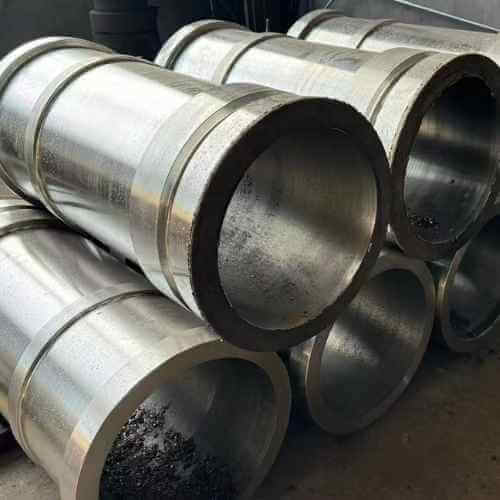
HK40 Alloy
25Cr-20Ni heat-resistant castings for ethylene cracking and standard furnace service.
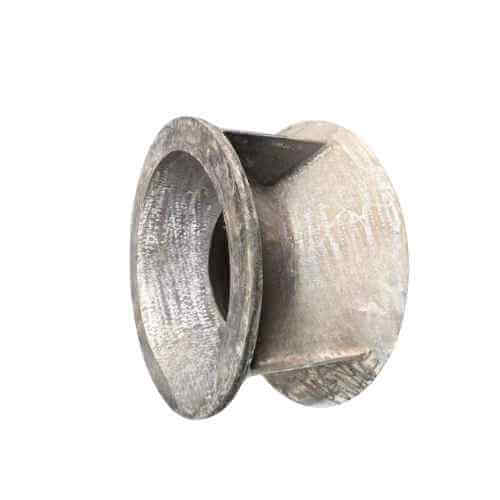
Inconel / Incoloy Castings
800H pigtails, outlet headers, severe-service nickel alloy components for refineries.
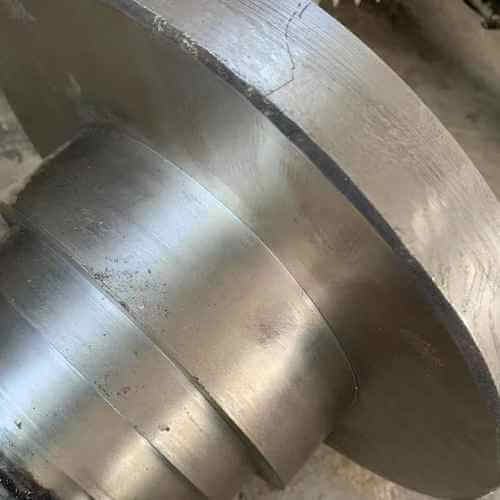
Process Tubes & Pipes
Stainless and alloy process piping for refinery and chemical plant downstream service.
Documentation that ships with every petrochemical order
What we deliver to EPC SQE teams and refinery procurement engineers.
Compliance documentation built alongside production — not after
Most centrifugal casting suppliers treat documentation as paperwork done after production. We build the package alongside casting: chemistry verified during melt, dimensional reports from first article, NDT during cooling cycle. EPC SQE teams receive a complete documentation package on the shipping date.
// Documents Shipped Per Order
Five-stage workflow from spec to shipped petrochemical casting
Engineering checkpoints between every stage. Nothing moves forward until the prior stage is signed off.
Spec Review
Project drawings, service conditions, and compliance requirements reviewed by engineering.
Sample & Approval
Pre-production samples shipped for EPC engineer signoff before bulk tooling.
Cast & Heat Treat
Centrifugal cast with verified chemistry, solution annealed per alloy specification.
NDT & Doc Pack
100% UT, pressure test, dimensional inspection. Full documentation package assembled.
Export Ship
Container loaded to project site or distributor warehouse with full paperwork pouch.
Petrochemical sub-industries we supply
Eight refining and petrochemical sub-verticals with specific tube and casting requirements.
Hydrogen Plants (SMR)
Steam methane reforming catalyst tubes for refinery hydrogen production.
Ammonia Plants
Primary reformer tubes for ammonia synthesis loops — 14m single piece.
Methanol Synthesis
Methanol converter tubes for methanol-from-syngas production.
Ethylene Crackers
Ethylene cracking furnace coils for steam-cracker pyrolysis service.
Propylene PDH
Propane dehydrogenation reactor tubes for propylene production.
Refinery Reformers
Catalytic reformer tubes for naphtha and BTX aromatic plants.
Delayed Coker
Coker furnace heater tubes with carburization resistance.
DRI Iron Plants
Direct-reduction iron reformer tubes for HBI/DRI feedstock.
Heat-resistant alloys stocked for petrochemical service
Material verified by spectrometer on every melt. Certificates per EN 10204 3.1 ship with every batch.
25Cr-35Ni
Standard reformer tube alloy. 1,050°C.
25Cr-35Ni + Nb
+15-25% creep. 1,150°C ceiling.
25Cr-20Ni
Ethylene cracking baseline. 1,100°C.
HK40 high-C
+15-20% creep over HK40.
15Cr-35Ni
Coker furnace carburization resistance.
19Cr-39Ni
Severe carburizing/sulfidizing.
Incoloy 800H
Pigtails, outlet headers.
Inconel 625
Severe corrosion + high-temp.
How we partner on petrochemical projects
Four phases from initial RFQ to delivered tubes — designed for refinery and EPC project timelines.
RFQ & DFM Review
Project specifications, service conditions, and compliance requirements reviewed by engineering team. Quote returned with material, dimensional, and certification scope.
✓ Quote · DFM · BOMSample & Approval
Pre-production samples shipped to EPC engineer for chemistry, dimensional, and metallographic approval. Compliance documents (mill cert, NDT report) included.
✓ Sample + CertProduction & QC
Batch production with in-process chemistry verification. Solution annealing per spec. 100% UT and hydrostatic test on every tube.
✓ FAI · UT · Mill certShip & Closeout
Containerized shipment to project site or refinery warehouse. Full compliance documentation pouch attached. Post-delivery quality support included.
✓ Compliance packSee how petrochemical castings get made
Three short videos covering reformer tube production, cracking tube casting, and pressure testing.

HP-Nb Reformer Tube Casting
14m single-piece HP-Nb reformer tube cast on horizontal centrifugal line at 1,200 RPM.
HK40 Cracking Tube Heat Treatment
Solution annealing at 1,150°C followed by rapid quench preserves cracking tube microstructure.
Hydrostatic Test & Documentation
1.5x design pressure hydrostatic test per ASME B31.3 with test certificate per tube.
Buyer questions on petrochemical casting service
Common questions from refinery procurement engineers, EPC project buyers, and hydrogen plant maintenance teams.