


Leading Centrifugal Cast Tubes & Pipes — 100-1,800 mm OD Stainless, Alloy & Heat-Resistant Grades
Kbear Metal manufactures centrifugally cast tubes and pipes in stainless steel, HP40, HK40, nickel alloy, heat-resistant, and wear-resistant grades. From 100 mm to 1,800 mm OD, up to 6,000 mm length, single-piece casting eliminates butt-weld failure points. ASTM A608 / A351 documentation per batch.
// Tube & Pipe Spec
Metrics that matter for industrial tube buyers
Hard numbers that define what we can supply for centrifugally cast tube and pipe projects.
Max Outer Diameter
Largest OD achievable on our horizontal centrifugal casting line.
Min Outer Diameter
Smallest economic OD. Below 100mm, seamless tube is preferred route.
Max Single-Piece Length
Eliminates butt-weld failure points common in fabricated pipes.
Max Tube Weight
Per-piece weight limit on our 1,800 mm bore casting machines.
Wall Thickness Range
From thin-wall pipes to heavy-section structural castings.
OD Tolerance
As-cast OD held within ±0.5 mm. Tighter via post-machining.
Alloy Families
Stainless, HP, HK, nickel, heat-resistant, wear-resistant, copper.
Lead Time (days)
Standard catalog tubes from confirmed PO to packed export crate.
Six tube and pipe configurations under one roof
Straight tubes, flanged, tapered, asymmetric — all cast as single-piece centrifugal castings.
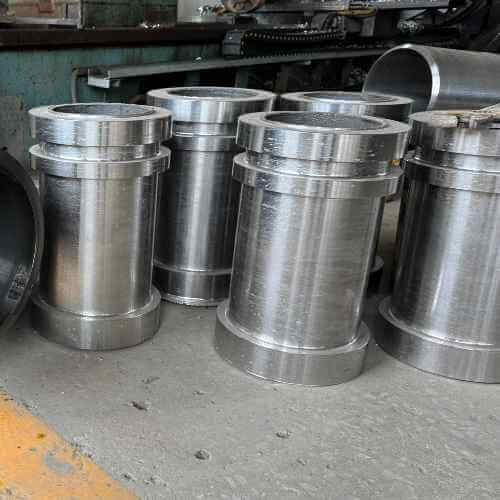
Flanged Straight Tubes
Pipeline tubes with integral cast flanges. Single-piece casting eliminates flange-to-pipe weld joints.
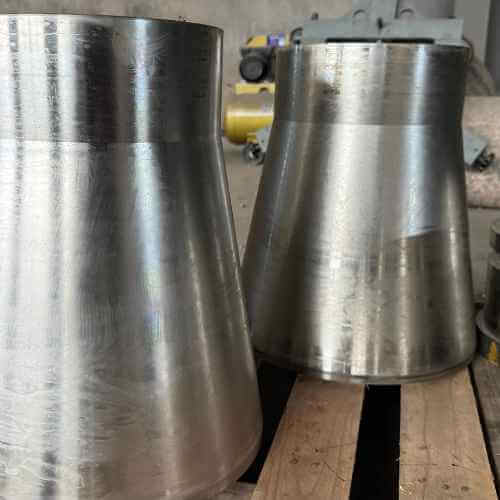
Tapered Tubes
Variable-OD tubes for transitions and adapter sections. Cast taper from 5° to 30° per side.
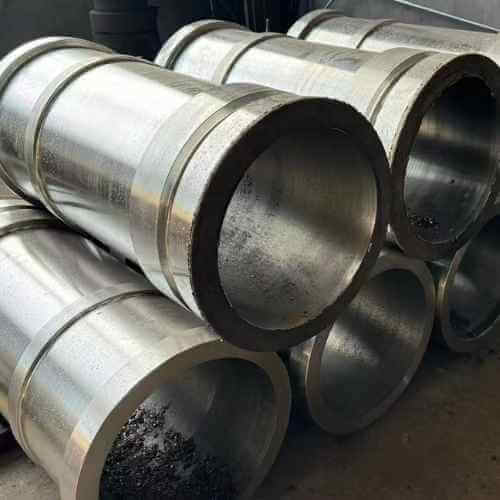
Standard Straight Pipes
Constant-OD process pipes for chemical, petrochemical, and high-temperature service.
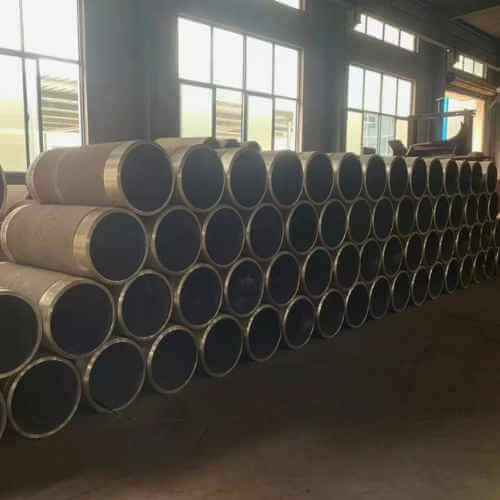
Heavy-Wall Tubes
Thick-wall tubes for pressure containment and structural service. Up to 150 mm wall thickness.
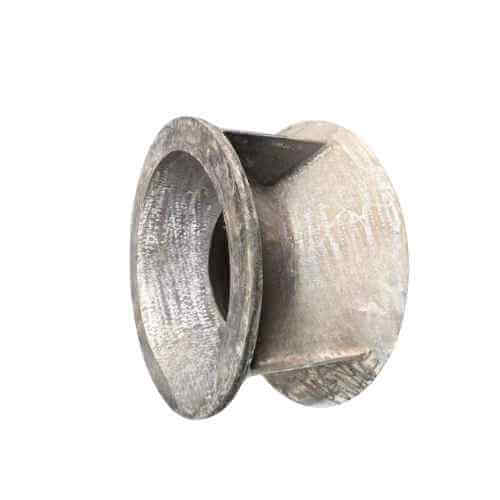
Special-Shaped Tubes
Asymmetric, multi-stepped, and complex-profile tubes cast as single piece from buyer drawing.
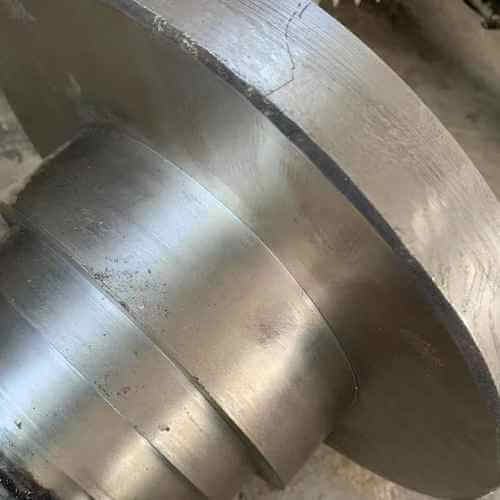
Hollow Bars
Heavy-OD hollow bars for further machining into rings, sleeves, gears, and bearing housings.
From melt to packed tube — eight controlled stages
Full documentation chain maintained from chemistry verification through final machining.
Drawing Review & DFM
Engineering reviews buyer drawing or sample. Material recommendation, mold design, and lead time returned in 48 hours.
Mold Prep
Sand or metal mold selected per OD, alloy, and quantity. Mold preheat 200-400°C, surface coating applied.
Melt & Chemistry
Induction furnace melts at 1,500-1,600°C depending on alloy. Spectrometer verifies chemistry pre-pour.
Centrifugal Pour
Mold at 200-1,500 RPM matched to OD. Tundish controls pour rate; centrifugal force distributes alloy.
Cooling & Demold
Controlled cooling profile prevents thermal cracking. Demold; ID rough-machined to remove impurity layer.
Heat Treatment
Solution anneal, normalize, or stress-relief per alloy spec. Documented thermal profile per batch.
NDT Inspection
UT, X-ray, dye-penetrant per ASTM E165/E709. Hydrostatic pressure test for pressure-service tubes.
Machine & Pack
OD/ID finish-machined to drawing tolerance, heat number stamped, end-protected, crated for export.
Seven alloy families for centrifugal cast tubes
Material verified by spectrometer on every melt. Mill certificates per EN 10204 3.1 ship with every batch.
Stainless 304H / 316L
Standard process piping, chemical service.
HP40 / HP-Nb
High-temp reformer and furnace tubes.
HK40 / HK45
Ethylene cracking, pyrolysis service.
Inconel 625 / 800H
Severe heat & corrosion service.
1.4848 / 1.4865
EU heat-resistant designations.
High-Cr Cast Iron
Wear-resistant tubes for mill rolls.
Aluminum Bronze
Marine, bearing, low-friction service.
Buyer-spec
Project-specific chemistry per drawing.
Centrifugal tube envelope by alloy family
Standard envelope. Custom dimensions and chemistry quoted on a project basis.
| Parameter | Stainless | HP/HK Alloy | Nickel Alloy | Wear-Resistant |
|---|---|---|---|---|
| OD Range | 100-1,800 mm | 80-350 mm | 100-800 mm | 200-1,500 mm |
| Wall Thickness | 10-100 mm | 8-25 mm | 10-80 mm | 30-150 mm |
| Max Length | 6,000 mm | 14,000 mm | 4,000 mm | 3,500 mm |
| Max Weight | 5,000 kg | 1,200 kg | 3,500 kg | 8,000 kg |
| Max Service Temp | 900°C | 1,150°C | 1,200°C | Wear duty |
| Surface Finish (Ra) | 1.6-3.2 μm | 1.6-3.2 μm | 3.2-6.3 μm | 3.2-6.3 μm |
| Standard Reference | ASTM A351 | ASTM A608 | ASTM A494 | ASTM A532 |
| Lead Time (days) | 25-40 | 35-55 | 40-60 | 30-50 |
Documentation chain that passes procurement audits
Industrial tube failures stop production lines. Our QC team builds the documentation package alongside production — chemistry verified before pour, NDT before machining, pressure tested before crating.
Spectrometer Chemistry
Every melt verified by ladle spectrometer before pour. Re-melt if off-spec.
100% UT Inspection
Ultrasonic on every tube — not statistical sampling. Defects flagged pre-machining.
Hydrostatic Pressure Test
1.5x design pressure per ASME B31.3 for pressure-service tubes.
Dimensional CMM
Coordinate measuring on first article and AQL sampling per shipment.
Heat Number Trace
Every tube stamped with heat number traceable to ladle sample and raw material certs.
Where centrifugal cast tubes ship from our factory
Eight industries where centrifugally cast tubes are the standard manufacturing route.
Petrochemical Process
Process piping for high-temperature refinery and petrochemical service.
Power Generation
Boiler tubes, superheater supports, gas turbine inlet components.
Steel Mill
Furnace roll shells, walking-beam furnace internals, slide-bearing sleeves.
Chemical Plant
Stainless process piping for chemical, pharmaceutical, food processing.
Cement & Mining
Kiln roller shells, mill liners, abrasion-resistant sleeves.
Glass Manufacturing
Glass plant furnace rolls, forehearth components, handling equipment.
Marine & Offshore
Aluminum bronze tubes for marine, offshore, and seawater service.
General Industrial
Hollow bar feedstock for downstream machining into rings, sleeves, gears.
See how a centrifugal cast tube gets made
Three short videos covering melt, casting, and quality verification at our Pingdu factory.

Stainless Tube Centrifugal Pour
304H stainless steel melt poured into mold spinning at 600 RPM. Centrifugal force distributes alloy.
Solution Anneal & Quench
Tubes solution annealed at 1,050-1,150°C per alloy spec, then rapid quenched for final microstructure.
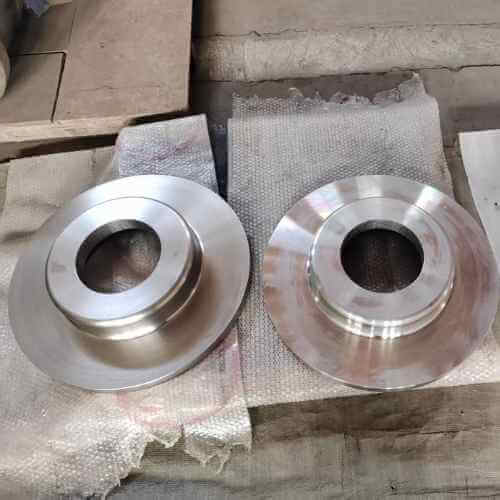
CNC Finish Machining
OD turned and ID bored to drawing tolerance, then heat number stamped and crated.
Buyer questions, answered directly
Common questions from process plant procurement teams, EPC project buyers, and tube fabrication shops.