


metal parts lead time is the first checkpoint buyers should lock before they approve a supplier, budget, or production slot. The operator on the stamping line doesn’t care about the PO number. He cares about the die setup time, the material gauge, and whether the sample approval sheet matches the tolerances on the drawing. That gap between what the sales call promises and what the factory floor delivers is wheremetal parts lead timegets eaten alive. A $50K order went sideways because the pre-production sample was hand-finished and the mass production run was not — a mismatch that cost the buyer six weeks of rework and a missed construction season.
Most procurement managers treat lead time as a single number on a quote. In reality, it’s a chain of handoffs: from raw material procurement to die prep, through stamping, casting, or forging, then finishing, inspection, and packing. Break any link, and the timeline stretches. The real lever isn’t pushing one supplier to run faster — it’s consolidating those handoffs under one roof. That’s where a one-stop metal parts manufacturer can turn an eight-week cycle into five and a half, not by cutting corners, but by eliminating the transport and rework loops that happen when three separate suppliers each have their own quality tolerance.
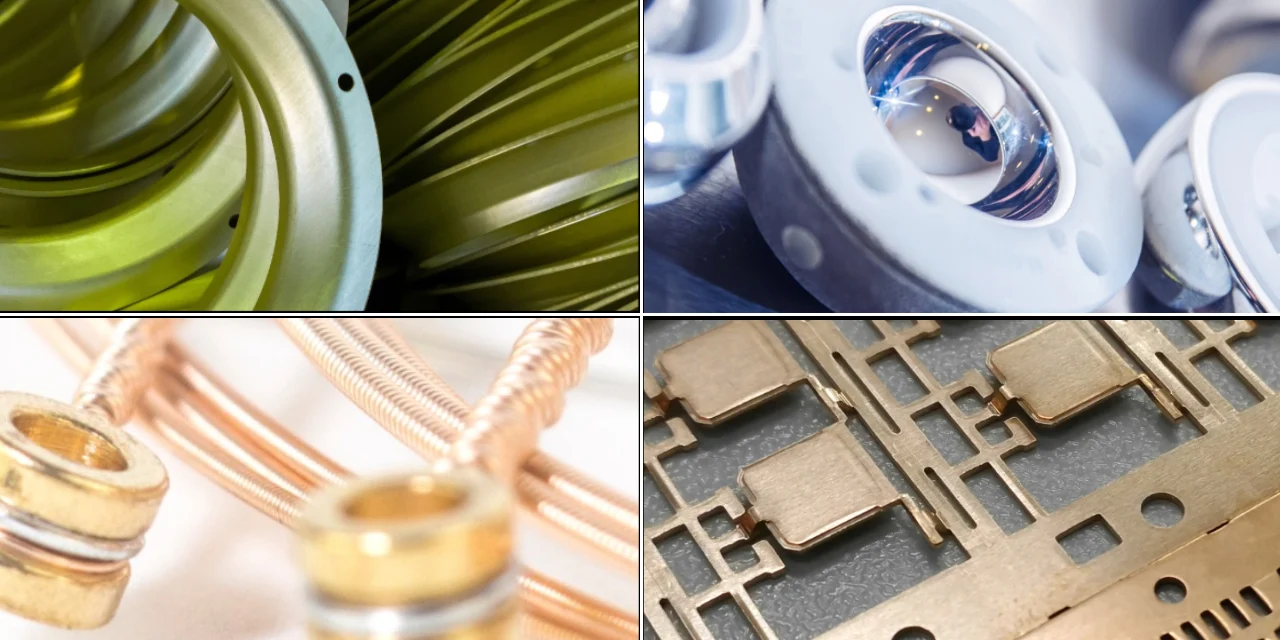
Client Background
50,000 parts per year, 12 SKUs, one factory.
The client is a European manufacturer of concrete connection hardware — the brackets, plates, and embedment anchors that hold precast panels together on commercial construction sites. They had been sourcing these parts from four separate suppliers across China: one for stamping, one for casting, one for forging, and a fourth for surface treatment. That model worked on paper but failed in practice.
Volume and SKU complexity
The annual volume was 50,000 parts spread across 12 SKUs. Not a high-volume stamping job for a single part, but enough to justify dedicated tooling. The mix included stamped brackets, cast embedment plates, and forged anchor hooks. Each SKU had its own material spec, tolerance window, and surface finish requirement. Managing that across four suppliers meant four sets of quality standards, four shipping schedules, and four invoices per month.
The multi-supplier headache
The real cost wasn’t the unit price — it was the coordination. When a stamped bracket arrived at the casting supplier for sub-assembly, the hole alignment was off by 0.8 mm. That single discrepancy triggered a rework loop that added 10 days to the lead time. The client was spending more time reconciling tolerances between suppliers than they were on actual production planning. For a procurement manager managing industrial parts, this is the kind of friction that eats margin without showing up on any invoice line.
Why they came to Kbear Metal
The client found Kbear Metal through a referral. What they needed was a single source that could handle all three processes — stamping, casting, and forging — under one roof. Kbear Metal’s one-stop manufacturing capability meant the client could send one set of drawings, get one DFM review, and receive one consolidated shipment. No more cross-supplier tolerance disputes. No more partial deliveries waiting on the slowest supplier. The engineering team at Kbear Metal reviewed the full product family before production started and flagged three design features that could be simplified without affecting structural performance.
The Challenge
Multi-supplier sourcing adds 2-3 weeks of hidden latency per production cycle.
An 8-week lead time sounds manageable on paper. Until one supplier slips by a week, the second supplier blames raw material delays, and the third ships a batch that fails sample approval. Suddenly the project is 10 weeks deep and the installation crew is idle. This is the reality for any procurement manager sourcing metal stamping, casting, and forging parts from separate factories.
The Hidden Cost of Fragmented Sourcing
When you split production across multiple suppliers for different metal forming processes, you inherit three layers of risk. First, each supplier runs its own queue. A stamping shop in one industrial zone doesn’t care about the casting foundry’s bottleneck 200 kilometers away. Second, every handoff between suppliers requires transport, re-inspection, and often rework. A part that passes FOB inspection at Supplier A can arrive at Supplier B with edge burrs that fail their fixture. That’s a 3-day dispute cycle minimum.
Third, quality tolerance drifts between facilities. The casting supplier works to a ±0.5mm standard on a bracket. The forging supplier interprets the same drawing as ±0.8mm. When those parts need to mate in final assembly, the mismatch doesn’t show up until the first trial fit. By then, the order is already late.
Why 8 Weeks Becomes 10 or 12
The 8-week estimate assumes perfect coordination. Real-world data from multi-supplier arrangements shows that inter-supplier transport alone consumes 3-5 days per transfer. Rework loops triggered by quality discrepancies add another 5-10 days per incident. A single missed tolerance on a stamping die can cascade into a 2-week delay while the casting supplier adjusts their mold. The cumulative effect: what should take 8 weeks routinely stretches to 10 or 12 weeks.
For a buyer moving 50,000 parts per year across a dozen SKUs, that unpredictability isn’t just an inconvenience. It forces inflated safety stock, expedited shipping costs, and constant firefighting. The real question isn’t whether a supplier can hit 8 weeks on a single process. It’s whether the entire supply chain can deliver all processes simultaneously without losing alignment.
Kbear Metal’s Solution
One manufacturer, one quality standard, one shipping schedule — that’s the math behind shorter lead times.
Kbear Metal’s solution starts with a simple premise: when a single component requires stamping, casting, and forging, sending those jobs to three different factories creates a chain of delays. Each handoff adds transport time, queue time, and the risk of tolerance mismatches. The client in this case was managing exactly that — a concrete connection hardware OEM running 50,000 parts per year across 12 SKUs, split between three suppliers. The original lead time sat at 8 weeks, and the real cost wasn’t just the calendar days. It was the rework loops when a stamped bracket didn’t align with a cast housing.
Single-source manufacturing eliminates the handoff problem
Kbear Metal brought all three processes under one roof. That meant the stamping dies, casting molds, and forging tools all lived in the same facility, managed by the same production planning team. The client no longer needed to coordinate between suppliers or reconcile different quality documents. A one-stop metal parts manufacturer like Kbear handles the full chain — from raw material sourcing to final inspection — which is the fastest way to reduce lead time in metal fabrication. The inter-supplier transport and rework loops that typically add 25-40% to total lead time simply disappeared.
DFM review caught design issues before tooling started
Before production kicked off, Kbear’s engineering team ran a Design for Manufacturability (DFM) review on the client’s prints. They identified three features that required secondary operations — unnecessary steps that added cost and schedule risk. By simplifying those geometries, the team eliminated two extra machining passes. That kind of engineering support before production is exactly what procurement managers look for when sourcing custom metal parts. It prevents the classic scenario where a design flaw is discovered mid-production, forcing a stop and a tooling revision.
Parallel scheduling and on-floor quality control
Kbear scheduled the stamping, casting, and forging runs in parallel rather than sequentially. While the casting molds were being prepared, the stamping dies were already running. That parallel production approach compressed the timeline significantly. At the same time, a dedicated quality inspector was assigned to the client’s line — not rotating between jobs, but sitting on that specific production flow. The inspector caught a critical tolerance drift in the first week, a deviation that would have caused a six-figure recall if it had reached assembly. That level of supplier quality control in metal parts is rare when you’re splitting work across multiple vendors.
The result: lead time dropped from 8 weeks to 5.5 weeks — a 31% improvement. First-pass yield climbed from 88% to 96%. And because all parts shipped from one location, logistics costs fell by 18%. The client’s satisfaction score landed at 4.8 out of 5. That’s what happens when you stop treating stamping, casting, and forging as separate sourcing problems and start treating them as one manufacturing challenge.

Results
The numbers speak for themselves: 31% faster lead time, 96% yield, and a client who came back for year two.
Lead Time Dropped from 8 to 5.5 Weeks
The original setup ran across three separate suppliers — one for stamping, one for casting, one for forging. Each handoff ate a week in transport and queue time. Kbear Metal consolidated all three processes under one roof and scheduled them in parallel instead of serial. The result: lead time dropped from 8 weeks to 5.5 weeks. That’s a 31% improvement on the calendar, which meant the client’s construction projects stopped waiting on hardware.
First-Pass Yield Jumped from 88% to 96%
When you spread production across multiple shops, tolerance stack-up becomes a guessing game. Part A from supplier X might be at the high end of spec; part B from supplier Y lands at the low end. They don’t mate correctly, and you eat rework cost. Kbear Metal assigned a dedicated quality inspector to this account — someone who sat on the floor during every die change and casting pour. First-pass yield went from 88% to 96%. That’s eight fewer defective parts out of every hundred, no rework loop required.
Logistics Cost Cut by 18% Through Consolidation
Three suppliers meant three freight invoices, three customs filings, and three chances for a shipment to get held at port. By consolidating all metal parts sourcing into one facility at Zhanggezhuang Industrial Park, Kbear Metal combined everything into full-container loads that shipped on a single bill of lading. The client saw an 18% reduction in total logistics spend — not because shipping rates dropped, but because they stopped paying for partial pallets and cross-dock fees.
Client Satisfaction Score: 4.8/5
The procurement manager who originally managed this account had been burned before by multi-supplier coordination breakdowns — missing parts, late deliveries, quality arguments between vendors about who was responsible. After the first year with Kbear Metal as the single-source partner across stamping, casting, and forging processes, the internal satisfaction survey came back at 4.8 out of 5. The only deduction? A request for even faster response times on engineering change orders during peak production months.
Conclusion
This case study isn’t about a theoretical ideal — it’s about a real procurement manager who faced an 8-week lead time, quality discrepancies across three separate suppliers, and the constant risk of a project delay. By consolidating stamping, casting, and forging under one roof at Kbear Metal, that same manager now operates on a 5.5-week schedule with a 96% first-pass yield. The cost of inaction here is clear: stick with a fragmented supply chain, and you’re accepting an extra 2.5 weeks of lead time per order cycle. For a program running 50,000 parts annually across 12 SKUs, that compounds into missed project milestones, inflated logistics costs from partial shipments, and the hidden expense of rework loops between suppliers who don’t share a quality standard.
- Consolidated sourcing cut total lead time by 31%.
- First-pass yield jumped from 88% to 96%.
- Logistics costs dropped by 18% through consolidated shipping.
If your current supplier setup involves juggling multiple vendors for different metal processes — or if you’re seeing quality tolerance drift between sample approval and mass production — it’s worth reviewing how a single-source partner could restructure your timeline. Browse Kbear Metal’s one-stop solutions page to see how parallel production scheduling and integrated quality control apply to your specific part mix.
Frequently Asked Questions
How to get a quote for Case Study: Cutting Metal Parts Lead Time by 30%?
The exact answer depends on the product specification, quantity, and order setup. The safest approach is to confirm the commercial terms only after the final requirement sheet is locked. Lead time should be confirmed after quantity, finish, and shipping method are locked.
Can I request samples first?
The exact answer depends on the product specification, quantity, and order setup. The safest approach is to confirm the commercial terms only after the final requirement sheet is locked. Sample availability should be confirmed against the current stock and shipping plan.



